
Welding & cutting / Buying guide
TIG vs. MIG vs. stick welding: which process fits the job?
Compare shielding, arc control, joint access and workflow for common shop and field welding jobs.
At a glance
Choose the welding process from material, joint access, shielding conditions, required quality and production pattern. MIG can suit repeated wire-fed fabrication, TIG offers separate control of arc and filler, and stick can suit supported field work. None is universally strongest; procedure and acceptance requirements determine the result.
- Process names describe electrode and shielding mechanisms; they do not establish a joint’s strength or fitness for service.
- Compare arc energy and job time with stated assumptions rather than ranking processes from amperage or bead appearance.
- A multiprocess purchase needs the right power, torch, gas, wire feeding and procedure support for every intended mode.
Quick answer
Choose MIG when speed, repeatability and an approachable learning curve matter for general shop fabrication. Choose TIG when precise heat control and a refined finish matter more than production speed. Choose stick when a supported electrode and procedure suit portable outdoor work; required surface preparation still applies. The machine’s documented capabilities still determine which materials and thicknesses it can handle.
How the three welding processes differ
Miller’s first-welder guide supports the fundamental distinctions: continuously fed wire for MIG, a nonconsumable tungsten for TIG, and flux-based shielding for stick and appropriate flux-cored processes. Those mechanisms explain workflow differences; they do not support declaring that one process always makes the strongest weld.
Joint design, material condition, filler, parameters and operator competence affect the result. For a load-bearing, lifting, vehicle or pressure-containing repair, obtain the applicable qualified evaluation and procedure. The process-comparison table is a purchasing aid, not authorization to carry out a consequential repair.
Choose the process, then qualify the setup
- 01Material + joint
- 02Environment + pace
- 03Supported process
- 04Power + consumables
At-a-glance welding process comparison
| Decision factor | TIG | MIG | Stick |
|---|---|---|---|
| Best known for | Control and clean appearance | Speed and repeatable shop work | Portability and field repair |
| Learning curve | Highest coordination requirement | Often the most approachable start | Arc length and electrode control take practice |
| Typical pace | Deliberate | Fast | Moderate with electrode changes |
| Outdoor wind | Shielding gas is vulnerable | Gas-shielded MIG is vulnerable; flux-cored setups vary | Generally well suited |
| Cleanup | Low when material is prepared well | Low to moderate depending on wire and settings | Slag removal is normally required |
| Portability | Gas and accessories add complexity | Wire feeder and possibly gas travel with the machine | Simple field setup with suitable electrodes |
The table describes broad process tendencies, not a capacity chart. Output range, polarity, AC or DC capability, wire or electrode type, shielding and accessories vary by machine.
Why the controls behave differently between processes
TIG uses a nonconsumable tungsten electrode, with filler added separately when needed. That separation lets the operator establish the puddle before adding filler. Its constant-current power source limits changes in current as arc conditions vary, making control different from conventional constant-voltage wire welding. TWI explains the TIG power-source characteristic.
In conventional MIG, the wire is simultaneously the electrode and the filler. Increasing wire-feed speed changes the amount of wire the arc must melt; voltage and other settings determine the operating condition. Stick also consumes its electrode, but the operator manually maintains arc length as the rod shortens and periodically replaces it. These physical differences explain why travel, filler addition, starts and cleanup occupy different portions of the job.
For comparison, do not use “150 A” as a complete description of any of these processes. Voltage, travel speed, transfer mode, electrode extension where relevant, filler and joint geometry all matter. An experienced operator may obtain a sound result with several methods, while an unsuitable procedure can fail with an expensive machine in any process.
How TIG welding works and where it excels
Tungsten inert gas welding uses a non-consumable tungsten electrode to form the arc. Filler metal, when needed, is added separately. The operator coordinates the torch, filler and often a foot or hand amperage control. That separation provides precise control over the heat and filler addition.
TIG is a strong choice for visible fabrication, thin material, stainless work and jobs where minimizing spatter is valuable. It rewards clean base metal and deliberate joint preparation. The tradeoff is pace: fit-up, cleaning and operator coordination generally make it slower than MIG.
Do not assume every TIG-capable machine welds every common metal. DC TIG is widely used for steel and stainless, while conventional TIG welding of aluminum usually calls for appropriate AC output. Also distinguish high-frequency starting from lift-start methods, and check whether a torch, remote control and regulator are included.
How MIG welding works and where it excels
Metal inert gas welding continuously feeds a consumable wire electrode through the gun. Once voltage and wire feed are set for the joint, the process can deposit metal quickly and consistently. This makes MIG productive for general fabrication, repair, automotive work and repeat assemblies.
MIG is often easier for a new operator to begin using because the machine feeds the electrode. Good results still depend on clean material, correct polarity, appropriate wire, shielding, sound settings and technique. Gas-shielded welding needs protection from drafts. Some wire-feed machines can run self-shielded flux-cored wire for outdoor or field conditions, but process support and polarity must be verified for the model.
For aluminum, check whether the machine supports the required wire-delivery arrangement, such as a compatible spool gun or push-pull system. “MIG capable” by itself does not confirm that aluminum accessories or programs are included.
How stick welding works and where it excels
Shielded metal arc welding uses a flux-coated consumable electrode. The flux provides shielding and leaves slag that is removed after the pass. Because the process does not require an external shielding-gas cylinder, a suitable stick setup can be compact and practical for outdoor maintenance, farm equipment and jobs that move around a site; load-bearing, lifting, vehicle and pressure-containing repairs require the applicable qualified evaluation, personnel and procedure.
Stick welding is generally more tolerant of wind and imperfect surfaces than gas-shielded TIG or MIG, but preparation and coating assessment must follow the material, consumable and applicable procedure. Electrode selection matters: different rods have different polarity, position, penetration, storage and base-metal requirements. Maintaining the arc and restarting cleanly take practice, and the process creates more smoke, spatter and cleanup than TIG.
Three jobs with different welding requirements
| Brief | Investigate first | Evidence needed |
|---|---|---|
| Repeated indoor steel assemblies | Productive wire-feed process | Wire/gas, power, rated duty and procedure |
| Small visible aluminum fabrication | AC TIG or appropriately equipped MIG | Documented aluminum support and representative result |
| Outdoor maintenance work | Supported stick or self-shielded FCAW | Electrode/wire restrictions, site power and hazard assessment |
Notice what is missing from the brief: a predetermined amp number and a universal winner. Start with material, access, repetition and quality requirements, then compare complete supported systems. If finish matters, ask for evidence from representative work. If output matters, compare duty cycle at the actual working current.
A technical comparison: arc energy per length
For steady conditions, arc energy in kJ/mm is 60 × arc volts × arc amps / (1,000 × travel speed in mm/min). Heat input may additionally include a process-efficiency factor; terminology differs between engineering conventions. TWI distinguishes arc energy from efficiency-adjusted heat input. State which quantity you are using instead of comparing incompatible numbers.
Calculated illustration: assume a steady 24 V, 150 A arc. At 300 mm/min, arc energy is 60 × 24 × 150 / (1,000 × 300) = 0.72 kJ/mm. At 200 mm/min it is 1.08 kJ/mm; at 400 mm/min it is 0.54 kJ/mm. These are invented steady operating points, not recommended parameters or measurements of TIG, MIG or stick machines.
This explains why a slower low-current weld is not automatically a lower-energy operation. It does not tell you that increasing travel speed is acceptable: fusion, bead geometry and the governing procedure still have to be satisfied. Nor does equal arc energy guarantee equal weld properties, since heat distribution, filler, thermal cycle and material response can differ.
For pulsed or rapidly varying waveforms, use the appropriate measured power or governing calculation method. Multiplying separately averaged voltage and current can miss their time relationship. A casual phone-video reading of the display is not equivalent to a documented procedure record.
Which process matches six common jobs?
| Job | Good starting point | Why |
|---|---|---|
| General steel shop fabrication | MIG | Productive wire feed and repeatable setup |
| Thin stainless with a visible finish | TIG | Fine control of heat and filler |
| Outdoor equipment repair | Stick | Portable setup and wind tolerance |
| Automotive panel work | MIG or TIG | MIG favors pace; TIG favors precise control |
| Aluminum fabrication | AC TIG or suitably equipped MIG | Choice depends on finish, thickness and production rate |
| One shop with varied repair work | Multiprocess | Several supported processes in one footprint |
Read beyond the process label
“Multiprocess” describes a family of capabilities, not a complete setup. Verify AC versus DC TIG, remote control, the wire-feeding arrangement and included accessories. The same power source may carry different output ratings by process; Miller’s Multimatic 235 specification is a clear example.
Use the duty-cycle worksheet and the power-supply checklist before comparing the price of two packages. For aluminum TIG, check AC/DC controls and torch support. For wire welding, check gas, polarity and wire compatibility. These are separate gates; passing one does not establish the others.
Compare the cost of an accepted part
Write a process trial as a whole job: prepare and fixture the part, weld it, remove required slag or spatter, inspect it and complete any finishing. Separate arc time from labor time. A method with faster travel may still lose its advantage if access is awkward, feeding interruptions occur or every assembly needs extra finishing.
Illustrative two-process screen: assume process A needs 4 minutes setup, 2 minutes welding and 3 minutes finishing/inspection per part: 9 minutes total. Process B needs 4, 4 and 1 minute respectively: also 9 minutes. At an assumed $60/hour station cost, both use $9 of time before consumables, rework and overhead differences. This is not a measured MIG-versus-TIG comparison; it shows why twice the arc speed need not halve the part cost.
Record accepted output, not just parts attempted. If a required weld must be inspected before it becomes inaccessible, include that hold point. If the shop changes material and process several times a day, include gas changes, wire/liner changes, torch changes and trial coupons. A shared multiprocess machine can save floor space while also becoming a bottleneck when two people need it simultaneously.
Use the catalog examples as candidates for a defined job. The wire/gas compatibility guide addresses changeovers, while the aluminum TIG guide covers waveform controls and representative trials. Neither a bundle photograph nor a process label proves the included setup meets the brief.
When a multiprocess welder makes sense
A multiprocess machine can reduce floor space and let a shop move between MIG, stick and one or more TIG modes. The label does not guarantee identical capabilities. Confirm the exact process combination, AC versus DC TIG, TIG start method, wire-feeder arrangement, spool-gun support and whether changing processes requires swapping leads, gas or internal components.
A combined machine is attractive when flexibility matters more than simultaneous operation. Dedicated machines may be preferable when multiple operators need to weld at once, one process dominates production or downtime on a single machine would stop all welding work.
Wind tolerance does not remove the hazard assessment
OSHA’s welding-fume guidance explicitly warns that outdoor work does not guarantee adequate ventilation. Identify base material and coatings, control exposures, and use the required fire, electrical and personal-protection measures. Preparation must follow the material, consumable and applicable procedure; contamination tolerance is not a reason to weld over unidentified coatings.
The products below are current catalog examples selected for topic relevance. We have not performed comparative weld tests, durability tests or procedure qualification on them. Verify each exact manual and package before deciding; model labels and seller photographs alone are not enough.
Power, duty cycle and workspace
Confirm the actual input voltage, phase, plug and circuit required. A dual-voltage machine may offer different output on each supply. Compare its documented amperage range with the work and review duty cycle at a relevant output. Duty cycle states how long the machine can weld within a defined test period before cooling; the test standard and ambient conditions matter.
Plan safe ventilation without directing drafts across a gas-shielded arc. Provide space for cylinders to be secured, leads to be routed, hot work to be isolated and flammable material to be controlled. Welding fumes, ultraviolet radiation, hot metal, electrical energy and compressed gas require appropriate training and protection.
Complete setup checklist
- Welder with the required process, material and output capability
- Compatible torch, gun, electrode holder and work lead
- Correct filler rod, wire or electrodes and replacement consumables
- Shielding gas, regulator and flowmeter where the process requires them
- Suitable electrical circuit, plugs or qualified installation
- Helmet with an appropriate shade, gloves, protective clothing and screens
- Fume control, fire prevention and a prepared work area
- Cleaning, fit-up and joint-preparation tools
TIG, MIG and stick welding questions
Which process makes the strongest weld?
The process name does not answer that. Strength and service performance depend on material, filler, weld size, fusion, defects, heat history and design. Compare a qualified procedure and its acceptance results for the intended joint, not appearance or a universal process ranking.
Can one multiprocess unit replace two simultaneous stations?
Only if simultaneous operation is explicitly supported by that equipment. Multiple process selections usually describe different operating modes, not independent output channels for two people. Include production scheduling and the consequences of one shared machine being unavailable when comparing it with separate stations.
Does a good-looking practice bead qualify a repair?
No. A surface view cannot establish internal fusion or suitability for a load-bearing application. Repairs involving lifting, vehicles, pressure or other consequential service need the applicable engineering evaluation, procedure and inspection.
Can I switch processes without changing the joint design?
Do not assume that. Access, root geometry, filler delivery, position and the required weld size can make a design suitable for one procedure but difficult for another. Review the complete joint and acceptance requirements before treating a process change as an equipment-only substitution.
Frequently asked questions
Which welding process is easiest to learn?
Many beginners find MIG the quickest route to a basic bead because the machine feeds the wire. Producing a sound weld still requires correct setup, joint preparation and practice. The best process to learn first is also the one that matches the work you intend to do.
Which process is best for thin metal?
TIG provides fine heat control, while a properly configured MIG machine can be productive on repeat thin-sheet work. The correct choice depends on alloy, joint, access and finish, and the selected machine must have a suitable low-end output and controls.
Can one machine weld steel, stainless and aluminum?
Some machines can, with the right process, polarity, output and accessories. Verify aluminum capability in particular; it may require AC TIG or compatible MIG wire-delivery hardware that is optional.
What should I compare after choosing the process?
Compare input power, useful output range, duty cycle, supported starting and feeding methods, included equipment, consumable availability, service support, size and total setup cost.
The product manual and current specifications control. Use welding equipment only within its ratings and with appropriate training, ventilation, fire controls and personal protection.
About this guide. AI-assisted research and editorial synthesis. It is not a hands-on product test or a substitute for the exact equipment manual, trained instruction or qualified installation advice. How we use sources.
Sources and references
The references below support the explanations and examples in this guide. Check the edition, model and test conditions when applying them to your equipment.
- Buying Your First WelderMiller Electric · Undated; accessed August 30, 2026
- Multimatic 235 specificationsMiller Electric · Undated; accessed August 30, 2026
- Guide to TIG Welding BasicsMiller Electric · Undated; accessed August 30, 2026
- What Type of Gas Is Best for MIG Welding in DIY Applications?Miller Electric · Undated; accessed August 30, 2026
- Controlling Hazardous Fume and Gases during WeldingOSHA · March 2013; US workplace context
- Tungsten inert gas welding: process and power sourceTWI · Accessed August 31, 2026
- What is the difference between heat input and arc energy?TWI · Accessed August 31, 2026
Product photographs and links refer to the existing Jumbo Industrial catalog. Verify specifications, included equipment and current availability on the live listing and in the manufacturer documentation.
Equipment for the job
Shop related equipment
Compare specifications, included accessories and installation requirements for your setup.

Related equipment
hynade TIG200GPACDC 200 Amp AC/DC Tig Welder – Dual Voltage 110/220V
Compare the exact supported processes, required accessories, rated output and changeover work against your joint and production brief. A multiprocess or aluminum label alone is insufficient.
View equipmentRelated equipment
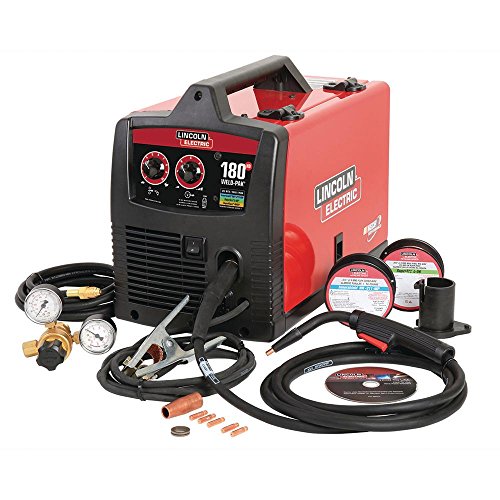
Lincoln Electric Weld Pak 180 Hd Red/Black
Compare the exact supported processes, required accessories, rated output and changeover work against your joint and production brief. A multiprocess or aluminum label alone is insufficient.
View equipment
Related equipment
LOTOS MIG175 175AMP Mig Welder with Mask, Solid Wires, Argon Regulator, Standard MIG Gun
Compare the exact supported processes, required accessories, rated output and changeover work against your joint and production brief. A multiprocess or aluminum label alone is insufficient.
View equipmentMore from the guide library
Related guides

Buying guide
Welder duty cycle explained: output, arc time and cooling
Read duty cycle alongside current, process and temperature to see whether a welder can handle your longest welds.
Read the guide
Buying guide
MIG gas and flux-core wire: shielding, polarity and compatibility
Match the wire and base metal with the right shielding gas, polarity, feeder parts and supported welding process.
Read the guideBuying guide
TIG welders for aluminum: AC/DC, controls and torch choice
Compare AC output, low-current control and torch options for the aluminum parts you plan to weld.
Read the guide