
Metalworking & machining / Buying guide
Mini-mill workholding: choose a vise that leaves room to machine
Fit the vise to the part and the mill, allowing enough travel, support and clearance for each cut.
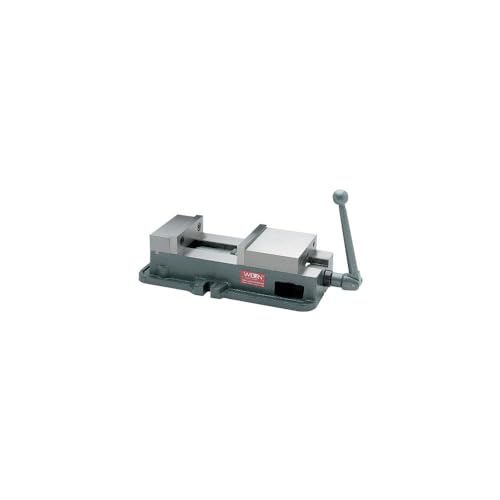
At a glance
Choose workholding around the part’s locating surfaces, cutting forces and tool access, then check the complete setup against X, Y and Z limits. A larger vise can reduce useful travel. Separate locating from clamping, and support the work so the required holding force does not distort it.
- The fixture must locate, support and restrain the work while leaving every tool path accessible.
- Jaw width alone does not describe vise fit, opening, height or load capability.
- Clamping harder can distort thin parts without solving a poor force path.
Start with the part, not the vise width
Lay out the recurring parts before choosing workholding. A rectangular block, thin plate and irregular casting place different demands on a fixture. Ask where the part can be supported, which faces must remain accessible and how cutting forces will be resisted. A vise that grips the stock may still obstruct the feature you need to machine.
On a mini mill, space is a real constraint. An oversized vise can consume Y travel, increase overhang and leave too little vertical clearance for the cutter. Choose the smallest suitable arrangement that securely supports the actual work; do not treat greater jaw width or weight as an automatic upgrade. LittleMachineShop’s tooling guide distinguishes vises, table clamping and supporting tools.
Build the fixture requirement from a drawing and an operation list. Identify the surfaces that establish location, the material removed at each stage and whether the same locating surfaces remain afterward. Removing the edge that a stop bears against can change the setup halfway through the job. A fixture review should therefore include the final state of the part, not only the starting stock.
Distinguish jaw width, maximum opening, jaw height and overall body size. These dimensions are not interchangeable. Two vises with the same jaw width can put the fixed jaw at different positions on the table and leave different cutter access. Also check mounting-slot compatibility and the travel required to reach the mounting hardware.
The support loop
- 01Machine table
- 02Vise / fixture
- 03Supported work
- 04Cutter + holder
- 05Spindle
Make a fit check in three directions
| Direction | Measure with the planned setup | Common surprise |
|---|---|---|
| X / left-right | Cutter reach over every feature | Part fits, but the final hole lies outside travel |
| Y / front-back | Jaw position, cutter centerline and column clearance | Vise body consumes useful reach |
| Z / vertical | Actual top-of-part height and tool projection | Drill or boring head cannot clear the part |
| Access | Handle swing, clamps and loading route | A clamp blocks the final operation |
The actual stack matters more than the sum of catalog heights. A workpiece can sit down inside a vise, so adding full vise height and full workpiece height can double-count the overlap. Measure from the table to the highest work surface in its supported position, then add tool projection and the clearance needed for the operation.
Locating and clamping do different jobs
Carr Lane’s fixture-design reference explains locating separately from clamping. The familiar 3-2-1 concept uses three contacts to establish a primary plane, two to orient a side and one to establish the remaining end position. Clamps retain contact with those references. This is a conceptual model, not a universal six-button fixture prescription for thin, curved or irregular work.
In a vise, the support surfaces, fixed jaw and an approved stop can serve analogous reference functions. A movable jaw supplies restraint, but its position is not automatically the best datum for the drawing. Identify which surface controls each critical dimension. If a second operation requires flipping the part, state which finished surface becomes the new reference and how the relationship is checked.
Overconstraint is another possible failure: if several contacts compete to establish the same location, a non-flat part may rock or distort as it is clamped. A useful fixture review asks which contact is intended to locate and which is merely supporting a flexible region. Adding more metal beneath the part is not automatically a better reference.
Clean seating is part of the setup
A chip under a vise or a burr under the part changes the reference surface before the cutter touches the metal. The University of Wisconsin’s mill teaching guide emphasizes clean contact surfaces, deburring, support and indicating the fixed jaw. These are useful preparation principles; its instructions for particular shop machines are not universal permissions for every mill.
Create a repeatable setup record: fixture identity, jaw or stop used as a reference, support arrangement, part orientation and the required alignment check. For a repeat job, a photograph of the stopped, safely prepared setup can be more useful than a sentence saying “clamp as usual.” It also helps another operator spot an omitted support or a changed clamp location.
Alignment error grows with feature spacing
Assume an ideal straight jaw is misaligned by 0.05 mm over a 100 mm indicated span. The small-angle estimate is θ ≈ 0.05/100 = 0.0005 rad. A feature 80 mm along that direction could have an illustrative transverse offset of 80 × 0.0005 = 0.040 mm. This isolates one geometric effect; it is not a complete machine error budget.
Whether that matters depends on the drawing. A loose stock cleanup and a tight rectangular hole pattern demand different evidence. Align the fixture to the operation’s requirement, and record the checked span rather than saying the vise is simply “square.”
Support the part against cutting forces
Ask what prevents the part from sliding, lifting or rotating under the planned cut. Unsupported thin stock may bend before it cuts cleanly. Long cutter projection or a tall fixture increases the opportunity for deflection. The answer is not always more clamp force: that may distort the workpiece or damage the fixture.
University research on large-overhang face milling by Xia and colleagues connects toolholder dynamics with the stable cutting region. It does not provide a performance gain for a benchtop vise. The useful engineering lesson is narrower: stiffness and overhang belong in the decision, and more motor power cannot correct a flexible setup.
A higher cutting point creates a larger overturning moment
For the same horizontal force, the moment about a reference is M = Fh. A hypothetical 100 N force acting 20 mm above a support plane creates 2 N·m; at 60 mm it creates 6 N·m. This explains why tall workholding changes the load path even when the cutter is unchanged. The assumed force is illustrative and cannot determine a required clamping torque.
A rating for the vise screw does not directly give the force retaining every workpiece. Jaw condition, geometry and support affect how loads reach the table. Kurt’s VersatileLock operating manual warns that off-center or above-jaw loading can cause jaw lift or loss of accuracy on the covered vise. Treat that as model-specific evidence to inspect the intended loading arrangement, not as a clamping recipe for another vise.
Why a thin part can look flat until you release it
A flexible plate can be pressed into a different shape during machining. If the cutter produces a flat surface while the part is bent, releasing the clamping load can change the finished geometry. Measure in the condition required by the drawing; an in-fixture result and a free-state result answer different questions.
Before blaming the mill, ask whether the work was supported beneath the cutting region, whether the clamp loads passed through those supports, and whether the part’s stiffness changed as stock was removed. A pocketed part can become substantially more flexible late in the operation. This is a reason to review the sequence and fixture with a qualified machinist, not to tighten the clamps until movement disappears.
| Symptom | Possible contributors | What to compare |
|---|---|---|
| Part changes after release | Elastic clamping distortion or residual-stress movement | Clamped and required inspection state; support and material history |
| Repeated parts sit at different heights | Chips, burrs, inconsistent seating or stock variation | Reference contacts and cleaning/seating records |
| An edge is tapered relative to a datum | Fixture alignment, part seating or cutting deflection | Datum setup, checked span and measurements at several locations |
| A final feature becomes inaccessible | Clamp interference or incomplete envelope planning | Every tool assembly and the full operation sequence |
Keep workholding and toolholding separate
The vise holds the work. The spindle holder retains the cutter. Both must be suitable. Confirm the spindle taper, drawbar/retention system and the cutter holder’s intended use. Do not substitute a drilling chuck for an end-mill holder unless the equipment manufacturer explicitly permits that application.
Before a cut, check the entire motion path with the machine in the safe setup state specified by its manual. Account for clamps, vise jaws, the table, tool length and the part at travel extremes. Never use hands to restrain a loose workpiece, and stop the spindle fully before measuring, changing the setup or clearing chips. Get supervised training for unfamiliar fixtures.
What to buy first
- A vise or fixture matched to the part, table slots, load and available travels.
- Compatible fasteners and clamping hardware—not improvised substitutes.
- Suitable parallels or support methods for the planned geometry.
- An indicator and mounting arrangement for alignment checks.
- Spindle-compatible holders and a restrained set of appropriate cutters.
- Deburring and chip-handling tools, plus the machine’s required guards and protection.
Compare the full setup in the benchtop mill buying guide. Then use the speeds and feeds guide to understand why a calculator needs correct tooling inputs. A well-held part is a prerequisite; it is not proof that any selected cut is within the machine’s capability.
Mini-mill workholding questions
Is a swivel base always worth the height it adds?
Only if its positioning function solves a recurring job and the resulting stack still fits. Account for the added interfaces, mounting footprint and height. If every planned operation uses the vise square to an axis, compare the actual benefit with the space it consumes.
Can I use a drill-press vise for milling?
Do not infer milling suitability from appearance or jaw width. Milling introduces the planned lateral and other loads throughout a toolpath. Use equipment explicitly suitable for the operation, with compatible mounting and an approved setup.
Why does an oversized vise reduce useful Y travel?
The table may still move its full mechanical distance, but the part’s position relative to the spindle and column can prevent the cutter reaching the required features. The body and jaw placement change usable access without changing the leadscrew travel.
Is a test cut enough to confirm a new fixture?
It gives evidence for that cut. Review restraint, tool access and support through the whole sequence, including entry, exit and the thinner final geometry. No single smooth cut proves that every later operation is suitable.
About this guide. AI-assisted research and editorial synthesis. It is not a hands-on product test or a substitute for the exact equipment manual, trained instruction or qualified installation advice. How we use sources.
Sources and references
The references below support the explanations and examples in this guide. Check the edition, model and test conditions when applying them to your equipment.
- Getting Started with Mini Mill ToolingLittleMachineShop · Undated; accessed August 30, 2026
- Eisen Mill GuideUniversity of Wisconsin–Madison ECB Shops · Updated January 13, 2025
- Chatter suppression in large overhang face milling using a toolholder with high dynamic performanceXia et al.; University of Strathclyde repository · May 30, 2020; DOI 10.1007/s00170-020-05515-3
- Guide to Locating and Clamping PrinciplesCarr Lane Manufacturing · Accessed August 31, 2026
- VersatileLock operating instructionsKurt Workholding · Accessed August 31, 2026
Product photographs and links refer to the existing Jumbo Industrial catalog. Verify specifications, included equipment and current availability on the live listing and in the manufacturer documentation.
Equipment for the job
Shop related equipment
Compare specifications, included accessories and installation requirements for your setup.

Related equipment
LittleMachineShop.com SIEG Mini Mill X2D 350W Variable Speed R8 Spindle Taper
Check the product page for specifications, included accessories and model details.
View equipmentMore from the guide library
Related guides
Buying guide
Choosing a benchtop milling machine: size, travel and rigidity
Check that the part, vise and cutting tools fit together, then compare usable travel, spindle performance and installation space.
Read the guide
Buying guide
Milling speeds and feeds: RPM, chip load and setup limits
Calculate spindle speed and feed rate from cutter data, then check chip thickness, tool reach and machine limits.
Read the guide
Buying guide
Calipers vs. micrometers: tolerance, accuracy and uncertainty
Choose a measuring tool for the feature and tolerance, with examples of temperature effects, alignment error and uncertain readings.
Read the guide