
Welding & cutting / Buying guide
MIG gas and flux-core wire: shielding, polarity and compatibility
Match the wire and base metal with the right shielding gas, polarity, feeder parts and supported welding process.

At a glance
Choose wire, shielding gas, polarity and transfer mode as one documented combination. Solid-wire MIG needs external gas; self-shielded flux core and gas-shielded flux core are different processes. A matching wire diameter alone does not establish that a spool suits your machine or joint.
- Wire classification and its exact data sheet govern polarity, shielding, position and application limits.
- More shielding-gas flow can create turbulence rather than improve protection; diagnose the complete gas path.
- Wire feed speed is not travel speed, and spool consumption is not the same as deposited weld-metal mass.
Solid wire, self-shielded and gas-shielded flux core
A wire-feed welder is not tied to one universal spool and gas bottle. Solid-wire MIG, self-shielded flux-cored wire and gas-shielded flux-cored wire are different combinations. “Flux core” does not always mean no external gas. The wire’s classification and data sheet determine the supported use, shielding and polarity.
Before changing a setup, record the exact wire name, diameter and spool format, the base metal and the machine model. Then check the manufacturer’s compatibility instructions. Reusing the old polarity or gas simply because the new wire fits through the gun can produce a fundamentally mismatched process.
Compatibility runs through the whole setup
- 01Base metal
- 02Wire specification
- 03Gas + polarity
- 04Feeding hardware
- 05Procedure
Common wire and shielding-gas combinations
| Work/process | Common starting point | Must be verified |
|---|---|---|
| Mild-steel short-circuit solid-wire MIG | C25: 75% argon / 25% CO₂ | Wire, transfer mode and machine guidance |
| Aluminum MIG | Commonly 100% argon | Alloy, wire feeding and compatible gun |
| Self-shielded FCAW | Wire supplies its own shielding system | Exact wire polarity and application restrictions |
| Gas-shielded FCAW | External gas specified for the wire | Do not run it as self-shielded wire |
| Stainless MIG | Wire/process-specific mixture | Do not copy a mild-steel gas choice |
Miller’s gas-selection guide identifies C25 as a common mild-steel choice and argon for aluminum MIG. Miller describes pure CO₂ as a lower-cost mild-steel alternative that can produce more spatter. A suitable argon-rich mixture may support spray transfer, but wire, machine and transfer mode must agree. Do not reuse a CO₂-containing mild-steel mixture for aluminum.
Gas also changes how the metal crosses the arc
In short-circuit transfer, the wire repeatedly contacts the weld pool. In spray transfer, droplets cross the arc without that repeated short circuit. Pulsed spray uses controlled current pulses to transfer droplets with lower average current than an otherwise comparable conventional spray condition. These are different operating regimes, not simply three names for turning the same voltage dial higher. TWI explains the transfer mechanisms.
For a purchasing decision, the key issue is whether the machine, wire and gas support the regime your procedure needs. A gas that works well for short-circuit steel welding should not automatically be treated as a spray-transfer gas. Likewise, a “pulse” button on a TIG machine is not evidence of pulsed MIG capability. Record the actual process name and supported wire/gas program when comparing multiprocess packages.
In conventional constant-voltage wire welding, wire-feed speed and current are linked by the burnoff behavior of the electrode; voltage helps determine the arc condition. Travel speed is how fast the operator moves along the joint. If a chart says 250 inches per minute of wire feed, that is not a 250 inches-per-minute torch travel instruction. Mixing the two can make a settings record impossible to reproduce.
Strict terminology calls steel welding with an active CO₂-containing shielding mixture MAG, while “MIG” is commonly used in shop and retail language for the broader wire process. Knowing both terms helps you find relevant manufacturer documents without assuming that instructions for inert-gas aluminum welding also apply to steel.
Read the application limits on the wire data sheet
Lincoln’s January 2018 NR-211-MP sheet describes that named self-shielded wire with DC electrode negative procedures. It also lists a 5/16-inch maximum plate thickness for the 0.030, 0.035 and 0.045-inch sizes. Those restrictions belong to that wire and revision; verify the current sheet before purchase.
This example matters because “use more passes” is not a blanket answer to a consumable’s application limit. Nor should its polarity be applied to every flux-cored wire. If an article, seller listing and spool label disagree, keep the machine off until the manufacturer resolves the exact combination. Store the resolved data sheet with the job information.
Check the parts between the spool and the arc
Wire diameter is only one fit check. The drive-roll type, liner, contact tip, gun and supported spool size need to match the wire and machine. Aluminum wire introduces its own feeding questions; a compatible spool gun or push-pull arrangement may be needed. Confirm the precise accessory part number and whether the package includes it.
For a buyer, the practical comparison is the cost of a complete supported setup. A low machine price can become less attractive after adding the required gun, regulator, consumables and cylinder arrangements. Conversely, a large accessory bundle adds little value if its contents do not suit the material you work on. Ask for an itemized list rather than judging the photograph.
Calculate wire consumption without confusing it with deposition
A simple geometry check helps plan spool use. For a solid round wire, cross-sectional area is πd²/4. Multiply that area by wire-feed speed and density to estimate the mass passing through the contact tip. The result describes wire supplied to the arc; spatter, start/stop losses and trimming mean it is not automatically the mass retained in a finished joint.
Illustrative solid-steel example: assume 0.9 mm diameter, 5 m/min wire feed and a density of 7.85 g/cm³. Area = π × 0.9² / 4 = 0.636 mm². Volume feed = 0.636 × 5,000 = 3,181 mm³/min = 3.181 cm³/min. Mass feed = 3.181 × 7.85 = 25.0 g/min, or about 1.50 kg per hour of arc time.
If this invented job has 20 minutes of wire feeding per clock hour, consumption is approximately 0.50 kg per clock hour before trimming and other losses. A 5 kg spool therefore represents about 3.3 hours of continuous wire feeding, not a promise of a particular number of finished parts or shifts.
Do not reuse this solid-wire density calculation for flux-cored wire. Its sheath, fill and effective density differ. Use the consumable supplier’s mass-per-length or deposition tables, keeping “wire consumption,” “deposition rate” and “deposition efficiency” separate. For cost comparison, divide measured consumable and labor cost by accepted parts rather than by the length of an attractive practice bead.
Wind resistance is not a fume-control plan
Gas shielding can be disrupted by drafts. Self-shielded wire may be a better process candidate for some outdoor work, subject to its application limits. That does not make any welding location automatically safe. OSHA’s welding-fume fact sheet warns that outdoor work does not guarantee adequate ventilation.
A shop also cannot solve fume exposure by blowing air indiscriminately across the weld. Fume control and shielding integrity must both be addressed. Coatings, confined areas and unfamiliar base materials warrant a proper hazard assessment and trained personnel. Do not use a change of wire as a substitute for identifying what is being welded.
A gas-flow reading does not prove shielding at the puddle
A cylinder regulator describes conditions at its measurement point. The gas still has to pass through hoses, valves, diffuser and nozzle before protecting the weld. A leak, obstruction or draft can make the puddle conditions different from what the gauge suggests. Excessive flow can also disturb shielding through turbulence; it is not a universal cure for porosity. TWI identifies leaks, drafts, excessive flow and moisture as distinct porosity causes.


| Symptom | First evidence to check | What it cannot prove alone |
|---|---|---|
| Porosity after a spool change | New wire identity, required shielding and surface condition | That the regulator needs more flow |
| Erratic feeding | Spool brake, roll/liner/tip match and gun routing | That voltage is wrong |
| Spatter after changing gas | Gas identity, polarity and matching process settings | That the power source is defective |
| Good appearance but failed acceptance test | Procedure, fusion, joint geometry and inspection findings | That a cleaner-looking process will be stronger |
Document the last known good combination before replacing anything. Test only within the approved procedure and manufacturer operating range. A repair to shielding does not establish that a previously porous weld is acceptable; the affected joint still needs its required evaluation.
Make a changeover card for each supported setup
- Base metal and the job’s applicable procedure or requirements.
- Exact wire name, classification and diameter.
- Gas specification, if needed, and manufacturer flow guidance.
- Polarity and supported transfer mode.
- Drive rolls, liner, contact tip and gun compatibility.
- Documented settings range, position and thickness restrictions.
- Cleaning, storage, ventilation and operator-protection requirements.
Keep the card beside the saved manufacturer documents. On a mixed-material bench it is a more reliable reminder than remembering the previous job’s settings. Use the welding-process comparison if the job does not clearly fit a supported combination; use the duty-cycle guide before assuming the machine can sustain it.
MIG gas and flux-core wire questions
Can I add gas to self-shielded flux core for better welds?
Do not assume so. Self-shielded wire is formulated for its specified environment. Adding external gas creates a different condition that the wire data sheet may not support. Buy the documented wire/gas combination required by the procedure instead of improvising a hybrid.
Can multiple passes overcome a wire thickness limit?
Not automatically. The NR-211-MP example above explicitly limits certain wire sizes by plate thickness. More deposited metal does not waive that restriction. A thick-to-thin joint also needs evaluation of both members, not just the thinner edge visible beside the bead.
Can I use my aluminum argon bottle for mild-steel solid-wire MIG?
A bottle being suitable for aluminum does not establish a supported steel transfer mode or weld result. Choose the gas specified for the exact wire and process. If you want one cylinder arrangement for several jobs, ask the supplier to document the supported combinations and compromises.
What belongs on a repeatable settings record?
Include base material, joint, wire name and diameter, gas, polarity, voltage or program, wire feed, travel speed, contact-tip-to-work distance and position. Add the actual machine and gun. This gives a technical reader enough context to assess the result while preventing an isolated voltage number from being mistaken for a universal recipe.
Compare the verified wire-feed examples in Welding & Cutting only after this combination is defined. The linked process guide helps when joint access or environment points toward a different method.
About this guide. AI-assisted research and editorial synthesis. It is not a hands-on product test or a substitute for the exact equipment manual, trained instruction or qualified installation advice. How we use sources.
Sources and references
The references below support the explanations and examples in this guide. Check the edition, model and test conditions when applying them to your equipment.
- What Type of Gas Is Best for MIG Welding in DIY Applications?Miller Electric · Undated; accessed August 30, 2026
- Innershield NR-211-MP data sheet, C3.2000.10Lincoln Electric · January 2018; verify current wire documentation
- Controlling Hazardous Fume and Gases during WeldingOSHA · March 2013; US workplace context
- Buying Your First WelderMiller Electric · Undated; accessed August 30, 2026
- What is MIG/MAG welding?TWI · Accessed August 31, 2026
- What is porosity and how can it be prevented?TWI · Accessed August 31, 2026
Product photographs and links refer to the existing Jumbo Industrial catalog. Verify specifications, included equipment and current availability on the live listing and in the manufacturer documentation.
Equipment for the job
Shop related equipment
Compare specifications, included accessories and installation requirements for your setup.
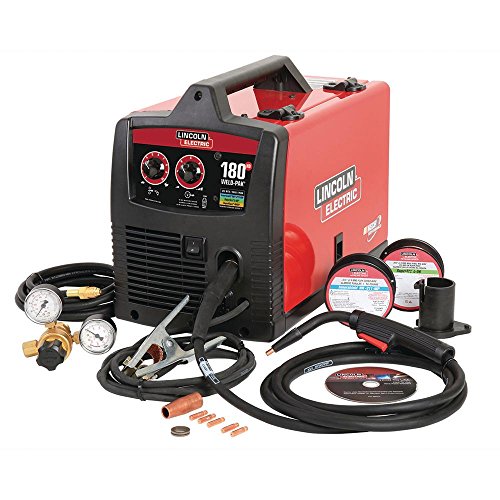
Related equipment
Lincoln Electric Weld Pak 180 Hd Red/Black
Check the supported wire classifications and diameters, gas connections, polarity changeover and gun/liner/drive-roll requirements for this exact package.
View equipment
Related equipment
LOTOS MIG175 175AMP Mig Welder with Mask, Solid Wires, Argon Regulator, Standard MIG Gun
Check the supported wire classifications and diameters, gas connections, polarity changeover and gun/liner/drive-roll requirements for this exact package.
View equipmentMore from the guide library
Related guides
Buying guide
TIG vs. MIG vs. stick welding: which process fits the job?
Compare shielding, arc control, joint access and workflow for common shop and field welding jobs.
Read the guide
Buying guide
Welder duty cycle explained: output, arc time and cooling
Read duty cycle alongside current, process and temperature to see whether a welder can handle your longest welds.
Read the guide